


Introduction
Blue tequila bottles, green olive oil bottles, brown Boston medicine bottles, and colorful candle jars—our lives are filled with vibrant glass packaging. Beautiful and unique, customers purchase these items to enhance their products, support their businesses, or decorate their homes and kitchens. Colored glass bottles serve a purpose beyond aesthetics; they play a crucial role in branding, packaging, and product preservation across various industries. They protect certain products from light exposure, which can lead to deterioration or failure.
While we often encounter a variety of colorful glass packaging, how are these stained glass bottles and jars made? For retailers and distributors, understanding the complexities of colored glass bottle production is essential for making informed purchasing and marketing decisions.
In this article, we will explore the composition of glass, the production processes involved in creating colored glass bottles, and their applications across different industries. We will also introduce Roetell Glass, highlighting the importance of our quality assurance and sustainable practices, providing retailers, wholesalers, and packaging distributors with exceptional quality that exceeds expectations.
Composition of Glass

What is Glass Made Of?
The foundation of glass lies in its basic components, which primarily include silica (silicon dioxide), soda (sodium carbonate), and lime (calcium oxide). Each ingredient plays a vital role in the properties of the finished product.
Silica: This is the primary ingredient in glass, typically derived from sand. Silica provides the structural integrity and clarity of glass. It melts at high temperatures, transforming into a viscous liquid that can be shaped and molded.
Soda: Sodium carbonate acts as a flux, lowering the melting temperature of silica. This makes the glass easier to work with, allowing manufacturers to produce glass at lower energy costs.
Lime: Calcium oxide is added to improve the durability and chemical resistance of glass. Lime helps stabilize the glass structure, preventing it from dissolving in water and enhancing its overall strength.
Role of Coloring Agents
The vibrant colors of glass are achieved through the use of coloring agents, which are primarily metal oxides. These agents can alter the way light interacts with the glass, producing a wide range of hues. Some common coloring agents include:
Cobalt Oxide: Produces a deep blue color.
Iron Oxide: Can create shades of green, amber, or brown depending on its concentration.
Manganese Dioxide: Used to produce purple and pink hues.
Copper Oxide: Yields turquoise or blue shades.
When incorporated into the glass during the melting process, these coloring agents bond with the glass matrix, ensuring that the color remains consistent throughout the bottle.
How Are Stained Glass Bottles Made
(1) Glass Bottles Manufacturing Process
The manufacturing of colored glass bottles involves several key steps, each requiring precision and expertise.
1. Melting the Raw Materials: The first step in producing colored glass bottles is melting the raw materials in a furnace. Temperatures typically exceed 1,600 degrees Celsius (2,912 degrees Fahrenheit). At this temperature, silica, soda, and lime melt to form a homogeneous molten glass.
2. Batching and Mixing: The raw materials are carefully measured and mixed to ensure a consistent composition. This step is crucial, as any variation can affect the color and quality of the final product.
3. Introducing Coloring Agents: At the appropriate stage in the melting process, coloring agents are added. The timing of this addition is critical; if added too early, the agents may not bond effectively with the glass, resulting in inconsistent colors.
4. Forming the Bottles: Once the glass is molten and the coloring agents have been incorporated, the glass is shaped into bottles. This is typically done using methods such as blow molding or press molding. In blow molding, air is introduced into the molten glass to expand it into a mold, while press molding involves pressing the glass into a mold to create the desired shape.
5. Annealing: After forming, the bottles are gradually cooled in a process known as annealing. This step is vital to relieve internal stresses and ensure the durability of the glass. Bottles are placed in an annealing lehr, where they are slowly cooled to room temperature.
(2) Color Technology
Color technology in glass production is a sophisticated process that enables manufacturers to achieve a wide range of shades and effects, enhancing both the aesthetic appeal and functionality of glass products.
Batch Coloring: This method is integral to producing colored glass bottles. It involves adding coloring agents directly to the batch of raw materials—such as silica, soda ash, and limestone—before the melting process. This technique ensures a uniform color distribution throughout the glass, which is critical for maintaining consistency in appearance and quality. The use of batch coloring is prevalent because it allows the color to be deeply embedded within the glass matrix. As a result, even if the bottle is cut, etched, or polished, the color remains intact, providing durability and longevity. This uniformity is essential for brands looking to maintain a consistent image and product presentation across their entire line.
Surface Treatment: Another approach to color application involves surface treatment, where a color coating is applied to the exterior of the glass after it has been formed. Techniques such as painting, spraying, or dip-coating are commonly used. While surface treatment can produce vibrant and eye-catching colors, it typically lacks the durability of batch coloring. Over time, the surface color may wear off or become scratched, which can detract from the product’s overall appearance and appeal. Consequently, while surface treatments can offer immediate visual enhancements, they may not be suitable for products requiring long-term durability and resistance to wear.
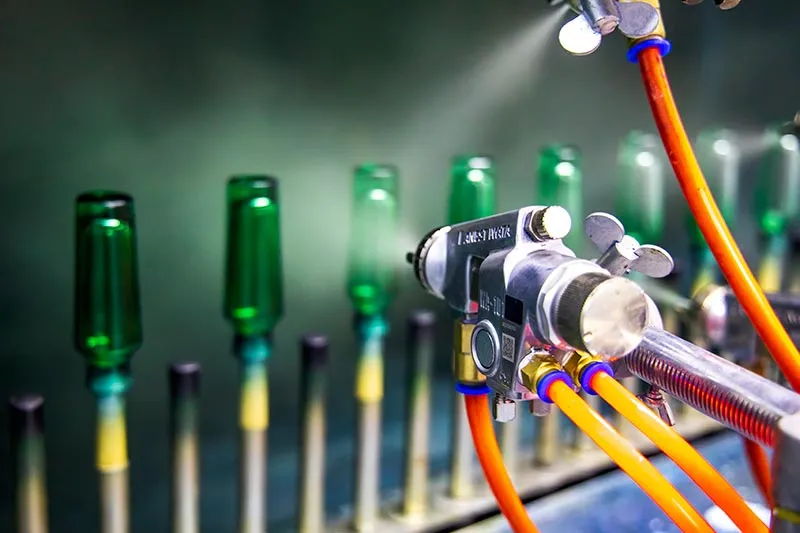
(3) Effect of Temperature
Temperature plays a crucial role in the glass-making process, particularly regarding color development and overall quality.
Impact on Color: Higher temperatures can significantly intensify the color of glass, resulting in brighter and more vivid hues. This enhancement occurs because increased heat promotes better mixing of coloring agents within the glass. Conversely, lower temperatures tend to produce softer, pastel colors, which may appeal to different aesthetic preferences. To achieve the desired color profile, manufacturers must carefully monitor and adjust the temperature throughout the melting and forming processes.
Temperature Control: Precise temperature control is essential not only for achieving color consistency but also for maintaining the structural integrity of the glass. Any fluctuations in temperature can lead to defects, such as bubbles or weak spots, compromising the final product’s quality and durability.
Applications of Colored Glass Bottles
(1) Industries Using Colored Bottles
Colored glass bottles find applications across various industries, each utilizing the unique properties of colored glass to enhance product presentation and functionality.
Food and Beverage Industry: Colored glass bottles are widely used in the food and beverage sector. For example, green and amber glass is often used for beer bottles and olive oil bottles, as these colors help protect sensitive contents from UV light that can degrade flavor and quality. Blue or milky white liquor bottles evoke an air of understated mystery, enhancing the brand image while aligning perfectly with the company’s high-end and sophisticated positioning.The global market for glass packaging in food and beverages is projected to grow significantly, reaching approximately $50 billion by 2025.
Cosmetics and Personal Care: The cosmetics industry frequently uses colored glass bottles for packaging perfumes, lotions, and serums. The aesthetic appeal of colored glass enhances the product’s luxury feel, making it more attractive to consumers. In this industry, the design and color of the packaging can significantly influence purchasing decisions.
Pharmaceuticals: In the pharmaceutical sector, colored glass bottles provide a barrier against light, ensuring the efficacy of sensitive medications. Amber glass is particularly popular for storing prescription medications, as it protects against UV exposure.

(2) Roetell Glass: Colored Glass Packaging Experts
At Roetell Glass, with over 39 years of experience in glass bottle manufacturing, we are committed to producing high-quality colored glass bottles that cater to the diverse needs of our clients across various industries. Our extensive expertise in glass manufacturing enables us to prioritize quality, durability, and aesthetics in every product. In addition to offering a range of colored glass bottles and jars, we also provide customization options to meet specific client requirements.
a. Examples of Products and Their Uses
Our product line includes a variety of colored glass bottles tailored for specific applications. For instance, we offer:
Wine Bottles: Available in green, amber, and clear glass, our bottles are designed to preserve the flavor and quality of wines.
Liquor Bottles: Crafted to showcase your premium spirits, our liquor bottles feature elegant designs that enhance shelf presence and brand identity.
Food Containers: Our colored glass jars are perfect for jams, sauces, and oils, combining practicality with visual appeal.

Cosmetic Jars: Stylish and functional, these jars are ideal for essential oils and lotions, enhancing the brand’s image.
Perfume Bottles: These exquisite perfume bottles are designed to reflect the luxury of your fragrance, adding a touch of sophistication to any product line.
Candle Jars: Perfect for scented or decorative candles, our jars combine aesthetics with functionality, making them an ideal choice for brands seeking to create a captivating ambiance.
b. Quality Assurance
Quality assurance is paramount at Roetell Glass. We implement rigorous testing protocols throughout the production process to guarantee that each bottle meets stringent industry standards for quality and safety. Our dedicated quality control team conducts regular inspections, focusing on key aspects such as color consistency, structural integrity, and surface finish. This meticulous approach ensures that every product not only meets but exceeds customer expectations, reinforcing our reputation for excellence in the glass manufacturing sector.
c. Sustainability of Production
Sustainability is deeply embedded in our production practices at Roetell Glass. We prioritize the use of eco-friendly materials and processes, striving to minimize waste and reduce energy consumption. Our commitment to sustainability not only enhances the aesthetic appeal of our colored glass bottles but also positions them as environmentally responsible packaging solutions. By integrating sustainable practices, we contribute to a greener future while providing high-quality products that meet the demands of today’s conscientious consumers.
Conclusion
The manufacturing process of colored glass bottles is a fascinating intersection of art and science. From the careful selection of materials to the precise control of temperature, each step is vital to producing high-quality products. At Roetell Glass, we are proud to offer a wide range of colored glass bottles that meet the diverse needs of retailers, wholesalers, and distributors.
By understanding how colored glass bottles are made, industry professionals can make informed decisions that enhance their product offerings and appeal to consumers. We invite you to explore our extensive range of colored glass products and discover how Roetell Glass can meet your packaging needs.