


In the manufacture of glass bottles and jars, the process of heating batch materials at high temperatures to form molten glass is called glass melting.
The tank furnace (or pool furnace) is the primary equipment used in glass plants for this process. It is constructed of refractory materials, typically featuring a rectangular structure with a large volume. Since glass tank furnaces operate continuously day and night, their full name is the “Continuous Glass Melting Tank Furnace,” or simply “tank furnace.” The tank furnace is the most critical and capital-intensive piece of equipment in a glass factory.
Types of Tank Furnaces
Currently, the following two main types of tank furnaces are used:
(1) Cross-fired Tank Furnace (also known as Side-fired Tank Furnace)
(2) Horseshoe-flame Tank Furnace (also known as End-fired Tank Furnace)
A brief description of the cross-fired tank furnace and the horseshoe-flame tank furnace is provided below.
Cross-Fired Tank Furnace
In a cross-fired tank furnace, several pairs of ports (or “small furnaces”) are symmetrically arranged on both sides of the melting end. When heavy oil is atomized by a nozzle for combustion, a large amount of combustion air is required. The ports serve as the outlets for this air and also as the exhaust ports for the high-temperature waste gas after the heavy oil combustion. The ports are also called burners.
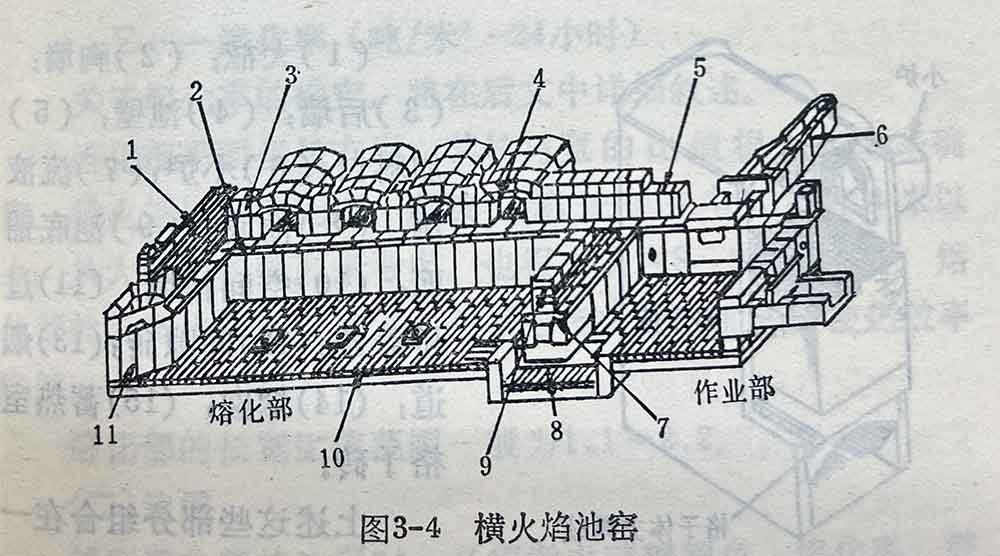
Figure 3-1 Schematic Diagram of a Cross-fired Tank Furnace 1 – Batch Charger 2 – Tank Block 3 – Main Crown 4 – Port 5 – Working End 6 – Regenerator Crown 7 – Checkerwork 8 – Regenerator Chamber 9 – Checkerwork Support 10 – Bottom Paving 11 – Melting End 12 – Flue
The regenerative heating method was invented by the Siemens brothers in Germany in 1857, which is why the cross-fired tank furnace is also known as the Siemens-type tank furnace. The cross-fired tank was first used to melt flat glass in 1873. The cross-fired tank furnace is suitable for mass production. Currently, tank furnaces equipped with regenerators are the most widely used in the glass industry.

Horseshoe-flame Tank Furnace
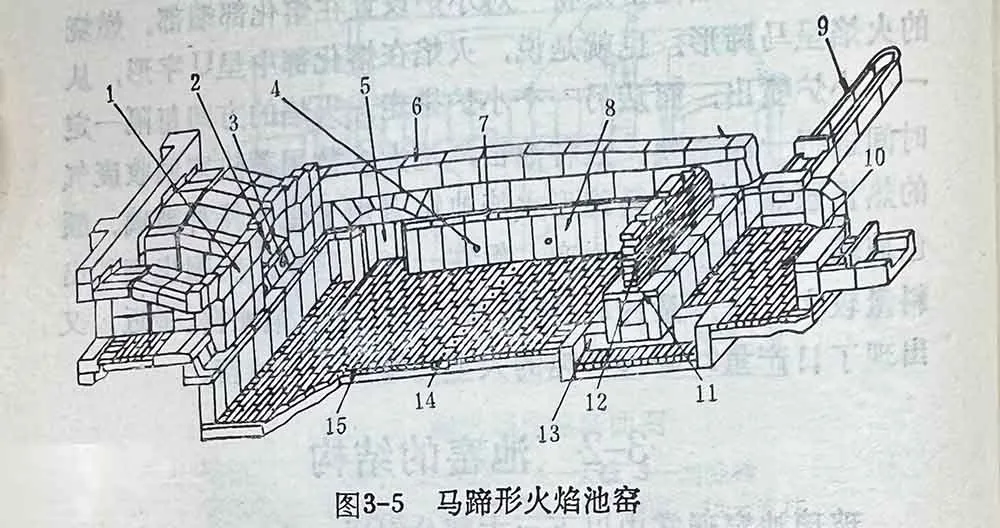
Furnace 1 – Port 2 – Melting End 3 – Skimmer Block 4 – Working End 5 – Throat 6 – Batch Charger 7 – Regenerator Chamber 8 – Flue 9 – Secondary Air Inlet 10 – Reversing Valve 11 – Chimney
The horseshoe-flame tank furnace has a pair of ports located at the end of the melting end. The combustion flame is horseshoe-shaped. That is, the flame forms a U-shape in the melting end, exiting from one port and exhausting through the other. The direction of the flame is reversed at regular intervals. Most of these furnaces use a regenerator to recover heat from the waste gas to preheat the air. The horseshoe-flame tank furnace is often used for producing special glass and colored glass, and is also suitable for small-scale production. However, in 1960, a horseshoe-flame tank furnace with a larger output, producing about 170 tons of glass per day, appeared in the United States. More recently, large-scale horseshoe-flame tank furnaces with a daily output of 200 to 300 tons have emerged.
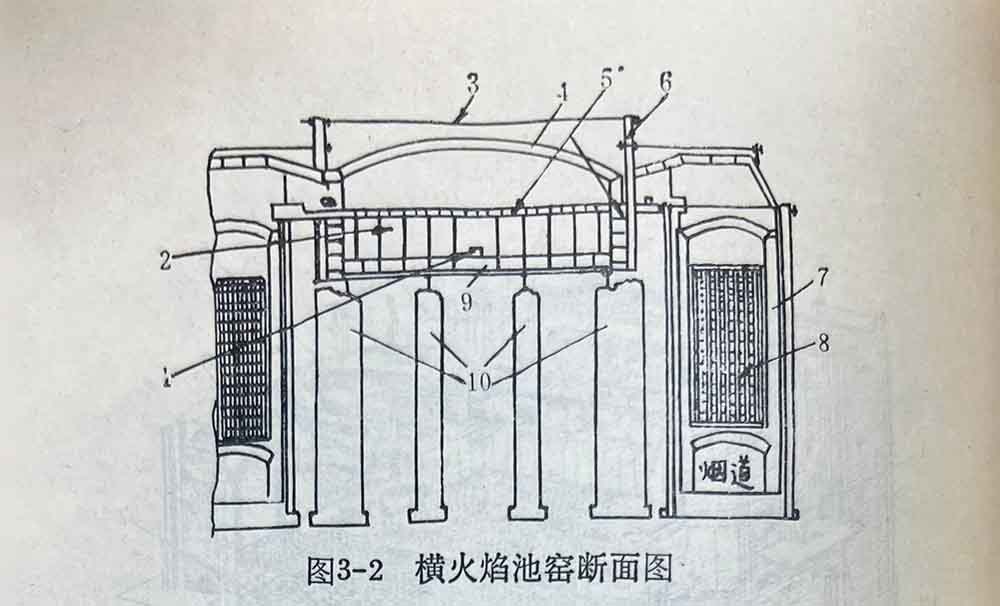
1 – Throat 2 – Tank Block 3 – Tie Rod 4 – Main Crown 5 – Tuckstone 6 – Furnace Wall Column 7 – Side Wall 8 – Checkerwork 9 – Bottom 10 – Support Column

Structure of the Tank Furnace
A glass tank furnace typically consists of the following three main parts:
(1) Melting End;
(2) Working End;
(3) Regenerator Chamber.
The names of the main parts of the tank furnace are shown in Figure 3-6.
1 – Back Wall 2 – Tuckstone 3 – Breast Wall 4 – Port 5 – Breast Wall 6 – Feeder Channel 7 – Bridge Cover Block 8 – Throat 9 – Skimmer Block 10 – Bottom Paving 11 – Batch Charger
1 – Back Wall 2 – Port 3 – Burner Block 4 – Electrode Port 5 – Batch Charger 6 – Breast Wall 7 – Tuckstone 8 – Tank Block 9 – Feeder Channel 10 – Working End 11 – Bridge Cover Block 12 – Skimmer Block 13 – Throat 14 – Bubbler Block 15 – Bottom Paving
(1) Main Crown; (2) Breast Wall; (3) Back Wall; (4) Tank Block; (5) Batch Charger; (6) Port; (7) Throat; (8) Bottom; (9) Bottom Paving; (10) Skimmer Block; (11) Bridge Cover Block; (12) Tuckstone; (13) Flue; (14) Chimney; (15) Regenerator Checker Bricks.
These parts, when combined, form a tank furnace. The main parts of the tank furnace are described below.
Melting End
The melting end is the most important part of the tank furnace. Its main function is to burn heavy oil, causing the added batch materials to melt into molten glass at a high temperature of 1500~1600°C and become fully homogenized. The molten glass then gradually decreases in temperature and flows towards the throat.
(1) Area
If the melting area is too large, heat loss increases, reducing the thermal efficiency of the tank furnace. If the melting area is too small, it can easily affect the quality of the molten glass, leading to a decrease in the yield of finished products. The area of the melting end can be determined by the following formula:
F = P/E
Where:
F — Melting end area (m²)
P — Output (tons/24 hours)
E — Melting rate (tons/m²·24 hours)
The determination of the melting rate will be described in detail later.
The melting end is rectangular in plan, and its length-to-width ratio is determined empirically. The width of a cross-fired tank furnace, considering the flame length, should be more than 4 meters; considering the strength of the main crown, it is rarely more than 8~9 meters. The length-to-width ratio of the melting end should not be too large, as this would increase the heat dissipation area and reduce thermal efficiency. The length-to-width ratio of the melting end generally ranges from 1.1 to 2.2.
(2) Depth
When determining the depth of the melting end, factors such as glass color, melting rate, bubbling, electric boosting, the temperature of the molten glass at the bottom paving blocks, and the degree of erosion of the paving blocks must be considered. The depth of the melting end for glass bottle and jar tank furnaces is about 0.9~1.5 meters; however, recently, there has been a trend towards increasing the depth. For tank furnaces melting colorless soda-lime glass, the depth can be determined by the following empirical formula:
Z = 0.4 + (0.5±α) log V
Where:
Z — Melting end depth (meters)
V — Melting tank volume (m³)
α = 0 ~0.135
For tank furnaces melting deep green glass, when the melting tank volume is 10~60 m³, the depth should be 0.2~0.3 meters shallower than the standard given by the above formula.
Working End
The molten glass, which has been melted in the melting end, flows into the working end through the throat. In the working end, the molten glass is further refined, eliminating small bubbles, and the glass temperature is adjusted to be suitable for the forming operation, allowing the molten glass to become a stable stream flowing into the feeder channel.
The ratio of the working end area to the melting end area varies depending on the type of glass. In glass bottle and jar tank furnaces, this ratio is about 5~30%.
The depth of the working end is generally shallower than that of the melting end to prevent the molten glass near the bottom from becoming too cold, which could lead to devitrification (crystal formation) in the glass body.
Regenerator Chamber
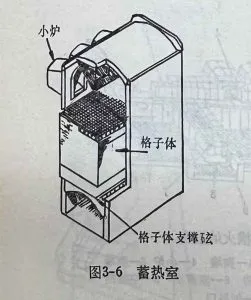
To ensure complete combustion of heavy oil, a large amount of preheated combustion air is required. The regenerator chamber is a heat exchange chamber that uses the heat recovered during its heat storage period to preheat the combustion air.
The preheated combustion air is called secondary air. In the melting end, the high-temperature waste gas resulting from heavy oil combustion causes a large amount of heat loss if it is directly exhausted through the chimney. If this heat is used to heat the secondary air, it is very beneficial for increasing the flame temperature, saving oil consumption, and improving the thermal efficiency of the tank furnace.
The regenerator chamber must have a sufficiently large volume. Inside the regenerator, checker bricks, which are slightly larger than the standard type, are stacked to form a checkerwork. The high-temperature waste gas heats the checker bricks that form the checkerwork. When the regenerator chamber reaches a very high temperature, cold air is introduced. The air is preheated as it passes through the regenerator and is then sent into the melting end through the ports to achieve complete combustion with the heavy oil atomized by the nozzle.
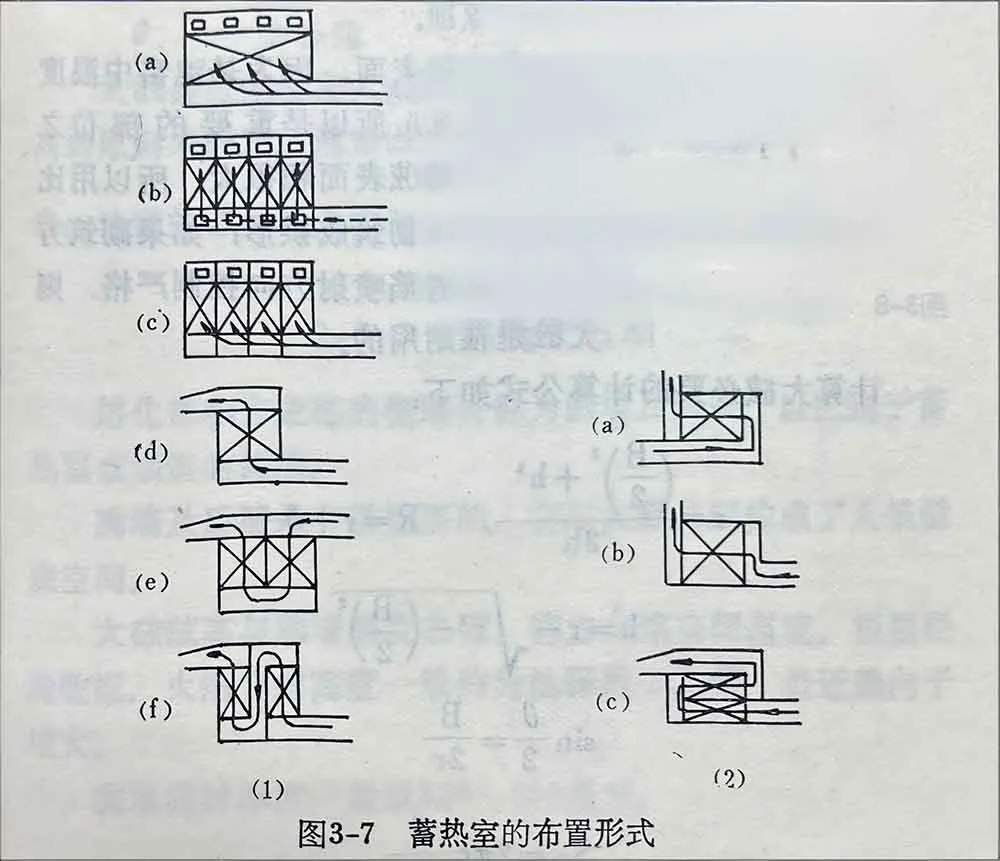
Since air cannot be introduced into the regenerator during the heat storage period (only waste gas can be introduced), the regenerator must consist of a pair of chambers so that the flow of air and waste gas can be reversed at regular intervals. During the reversal, the burners are temporarily shut off, which has a minimal impact on the furnace temperature.
(1) Vertical Regenerator (2) Horizontal Regenerator
Regenerators are classified into two types—vertical regenerators and horizontal regenerators—based on the flow direction of the secondary air or exhaust gas. The commonly used configurations are shown in Figure 3-7.
Horseshoe-fired (end-fired) tank furnaces are equipped with one pair of regenerators. Cross-fired tank furnaces, due to their larger furnace size and multiple pairs of ports, have correspondingly larger regenerators.
Secondary air can be preheated to approximately 1300–1350°C within the regenerator.
Crown
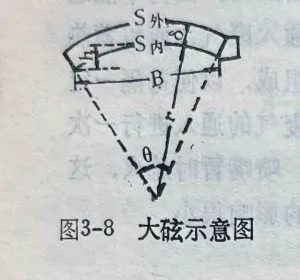
The arched roofs over the melting zone and the working zone are collectively referred to as the crown, in order to distinguish them from the roofs of the regenerators or flues.
Because the inner surface of the crown is exposed to the highest temperatures within the tank furnace, it is one of the most critical structural components. Due to its large surface area, the crown is constructed as an arch using relatively small refractory bricks. When the masonry method is properly executed and the flame direction is strictly controlled, the crown is highly durable and has a long service life.
The formulas required for calculating the crown are as follows:
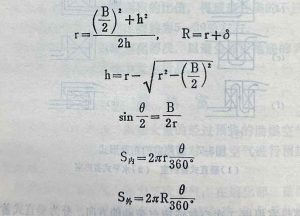 Where: R — Outer radius of the main crown
r — Inner radius of the main crown
δ — Thickness of the main crown
B — Span of the main crown
S内 — Inner arc length of the main crown,
S外 — Outer arc length of the main crown
h — Crown rise
θ — Center angle
The thickness of the main crown bricks and the crown rise are determined based on the principles of minimizing heat loss and maximizing structural strength. The thickness of the main crown bricks in a tank furnace is generally 300~350 mm; the ratio of the crown rise to the main crown span (h/B) is generally 1/8 ~1/10.
Breast Wall and Back Wall
The side walls of the melting end and the working end are specifically called the Breast Wall and the Back Wall to distinguish them from the side walls of the regenerator or the flue.
The breast wall and back wall are very important, as they, together with the main crown, form the space for flame combustion.
The sum of the crown rise and the height of the breast wall is called the flame space height. Based on empirical data, the flame space height is generally about 1.2 times the tank depth, and there is a recent trend towards increasing this height.
The thickness of the breast wall bricks is generally 300~500 mm.
Port
The main function of the Port is to eject the secondary air, allowing the air to mix quickly with the atomized oil droplets for rapid combustion and to achieve the desired flame. The port also serves as the exhaust outlet for the waste gas after the heavy oil combustion.
The installation position of the oil burner nozzle in the port is shown in Figure 3-9. The method shown in the figure, where the oil burner nozzle is installed below the port opening, is the most common one used in glass factories today. The advantages of this method are: (1) the flame is close to the glass surface; (2) the flame coverage is large; (3) the nozzle does not directly contact the high-temperature gas flow; (4) the nozzle is easy to operate.
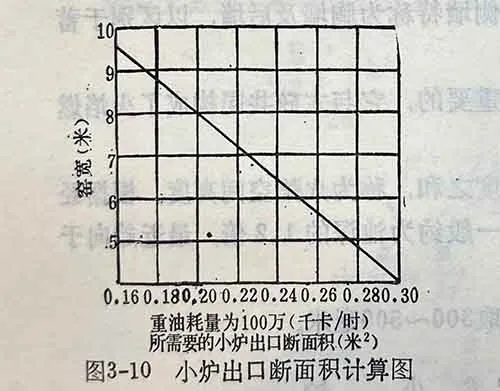
Once the dimensions of the tank furnace melting end are determined, the cross-sectional area of the port outlet can be determined based on the fuel consumption. Figure 3-10 shows the cross-sectional area of the port outlet for a fuel consumption of 1 million (kcal/h). In the figure, the furnace width for a cross-fired tank furnace refers to the distance between the outlets of each pair of ports in the melting end; for a horseshoe-flame tank furnace, the furnace width is calculated by multiplying the distance between the port outlet and the skimmer block by 1.5.

Batch Charger
The Batch Charger is the place where the batch materials are introduced into the melting end of the tank furnace. To facilitate charging, the batch charger slightly extends outward from the melting tank.
The function of the batch charger is: to keep the charging machine away from the high-temperature zone to prevent heat damage; and to pre-melt the batch materials to reduce the phenomenon of carry-over (flying material).
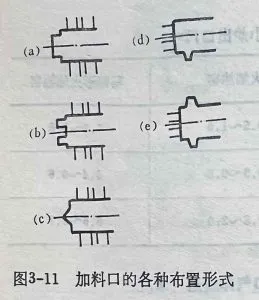
In a cross-fired tank furnace, the batch is charged at the back wall of the melting end, and the arrangement of the batch charger is shown in Figure 3-11 (a, b, c). In a horseshoe-flame tank furnace, the batch is charged at the side wall of the melting end, and the arrangement of the batch charger is shown in Figure 3-11 (d, e).
Throat
The Throat is located between the melting end and the working end. It is a tunnel with a small cross-section that connects the molten glass flow in the melting end and the working end.
The flow of molten glass from the melting end encounters significant resistance near the throat. Most of the molten glass is blocked and flows back, and only a portion of the high-quality molten glass passes through the throat into the working end.
The throat serves to remove bubbles and to reduce the temperature of the molten glass.
The relationship between the throat dimensions and the output of the tank furnace is shown in Table 3-3.
Table 3-3 Relationship between Throat Dimensions and Tank Furnace Output (Table)
Throat Height × Width (cm) | Tank Furnace Output (tons/24 hours) |
15 × 30 | 6 ~ 8 |
20 × 40 | 10 ~ 12 |
30 × 45 | 12 ~ 40 |
30 × 60 | 40 ~ 120 |
For tank furnaces melting colorless soda-lime glass, the throat dimensions can also be calculated using the following approximate formula:
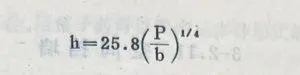
Where:
h — Throat height (cm)
b — Throat width (cm)
P — Output (tons/24 hours)
Tank Block
The surrounding brick walls that are in direct contact with the molten glass in the melting end and the working end are called the Tank Block.
Because the tank block is in direct contact with the high-temperature molten glass, it is one of the most important parts of the tank furnace.
The area where the tank block bricks meet the molten glass surface is the most susceptible to erosion and damage, which is usually the weak point of the tank furnace and the main reason for cold repairs.
The tank block is constructed by vertically arranging large bricks, which typically have dimensions of 250 mm x 450 mm x 900~1500 mm.
Bottom
The bottom of the tank furnace that holds the molten glass is called the Bottom.
The bottom is a very important part of the tank furnace.
As the output of the tank furnace increases and the campaign life extends, the erosion of the bottom by the molten glass intensifies.
Using clay blocks for the bottom can no longer meet the requirements. Therefore, a method of lining the bottom has been adopted, which involves laying a layer of high-performance bricks, called bottom paving blocks, with a thickness of 75~150 mm on the surface of the bottom.
Bricks with slightly inferior performance can be used for the construction beneath the bottom paving blocks. To reduce heat loss, insulating bricks are laid beneath these bricks.
Skimmer Block
The brick wall that separates the flame space of the melting end and the working end is called the Skimmer Block.
Because the temperature of the melting end is very high, the temperature of the working end must be lower than that of the melting end. To prevent the high-temperature flame from the melting end from entering the working end, and to prevent the influence of high-temperature radiant heat on the working end, a skimmer block is built with bricks between the working end and the melting end.
If the skimmer block completely prevents the flame and heat from the melting end from entering the working end, the temperature of the working end may become too low. Therefore, in both horseshoe-flame and cross-fired tank furnaces, the construction of the skimmer block leaves a small gap.
Recently, due to the increase in the melting rate of tank furnaces, the molten glass entering the working end from the melting end carries more heat, which tends to raise the temperature of the working end. At the same time, to prevent the erosion of the refractory materials in the working end by carry-over from the melting end and to facilitate the temperature adjustment of the working end, the skimmer block tends to be built as a sealed wall.
Tuckstone
The bricks laid on top of the tank block bricks at the top of the tank wall are called Tuckstones.
The functions of the tuckstone are: (1) To prevent the flame from the melting end from directly contacting the top of the tank block bricks; (2) To prevent silicate melt corroded from the breast wall or main crown from falling onto the top of the tank block bricks.
Regenerator Checker Bricks
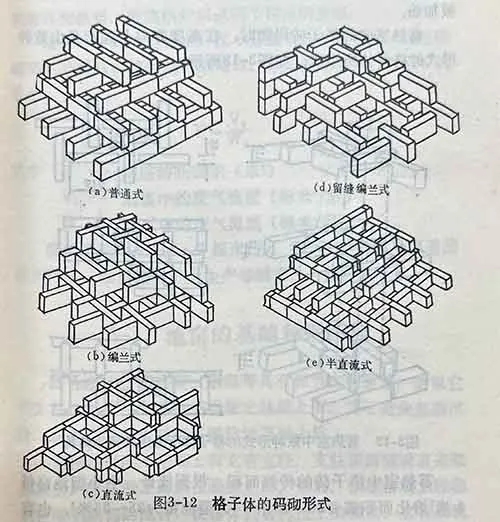
The large number of bricks stacked vertically in the regenerator chamber to form the checkerwork are called Regenerator Checker Bricks. Various forms of checkerwork can be built with checker bricks, as shown in Figure 3-12.
Because the checker bricks in the regenerator chamber are stacked very high, and the checker bricks are prone to clogging by glass powder and damage, the type of checker bricks needs to be carefully considered.
When the checker bricks in the regenerator chamber are heated by waste gas during the heat storage period, the temperature of the upper checkerwork is about 1300~1500°C, and the temperature of the lower part is about 600°C. When the checker bricks in the regenerator chamber release heat, cold air is drawn in from the bottom of the regenerator and is heated as it passes through the checker bricks.
When stacking the checker bricks in the regenerator chamber, the structure is usually composed of several forms of checkerwork in the vertical direction, as shown in Figure 3-13.
According to statistics, the heat transfer area of the checker bricks in the regenerator chamber required per 1 m³ of melting area is 20~25 m² for small and medium-sized tank furnaces, and 25~35 m² for large tank furnaces, with some reaching 40 m². If the temperature of the waste gas entering the checkerwork is 1350°C, the flow velocity of the waste gas in the checkerwork is 1.6~3 m/s.

Flue
The waste gas exiting the regenerator chamber is discharged through the chimney via the Flue. The flue is equipped with a reversing valve, a waste heat boiler, and a damper for regulating the furnace pressure.
The cross-section of the flue should not be too small, as a small cross-section can easily cause an increase in furnace pressure, which affects the increase in furnace temperature and shortens the life of the tank furnace. The cross-sectional dimension of the flue can be calculated by the following formula:
F=V0 /W0
Where: F — Cross-sectional area of the flue (m²)
V0 — Flow rate of the waste gas in the flue (standard m³/s)
W0 — Flow velocity of the waste gas in the flue (standard m/s)
The flow velocity of the waste gas is generally taken as 1~3 standard m/s. Considering the severe accumulation of ash in the flue during the later stage of production and the possibility of expanding the tank furnace production, the lower limit is generally chosen.