


Tank Furnace Foundation and Steel Structure
Because the furnace body, regenerator chamber, chimney, etc., have considerable weight, they are mostly built on a reinforced concrete foundation. To prevent foundation settlement, concrete piles are set beneath the reinforced concrete foundation.
On the reinforced concrete foundation, support columns are erected. Main beams and cross beams are set on top of the support columns, and the furnace body is built on top of the cross beams. Then, with the cooperation of steel structures such as furnace wall columns and tie rods, the furnace body achieves structural strength. The reinforcement of the regenerator chamber, which is built directly on the reinforced concrete foundation, is done in the same way. For other relevant parts, the selected steel components should be adapted to the shape and size of that part.
The calculation formula for the main crown and the steel structure on the side of the furnace is as follows:
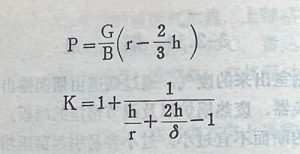
Where:
P — Horizontal thrust of the main crown when not heated
G — Weight of the main crown
B — Span of the main crown
r — Radius of the main crown
h — Crown rise
K — Correction factor for the increase in thrust when heated
δ — Thickness of the main crown
Main Auxiliary Devices of the Furnace
Oil Burner Nozzle
The Oil Burner Nozzle is a device that atomizes heavy oil for combustion. The main types of oil burner nozzles used in tank furnaces are as follows:
(1) External Mixing Stream Type Oil Burner Nozzle
This type uses a high-pressure air stream (compressed air) or superheated steam stream outside the nozzle to atomize the heavy oil (see Figure 3-14). The compressed air or superheated steam used to atomize the heavy oil is called the atomizing medium, and its consumption varies depending on the nozzle. When the atomizing medium is compressed air, the consumption of compressed air per 1 kg of heavy oil is 0.3~0.8 standard m³ of oil consumption; when the atomizing medium is superheated steam, the consumption of steam per 1 kg of heavy oil is 0.2~0.6 kg. The pressure of the atomizing medium is generally about 3~5 kg/cm², and the pressure of the heavy oil is slightly lower than this value. The compressed air used to atomize the heavy oil is also called secondary air; the primary air not only atomizes the heavy oil but also participates in the combustion.
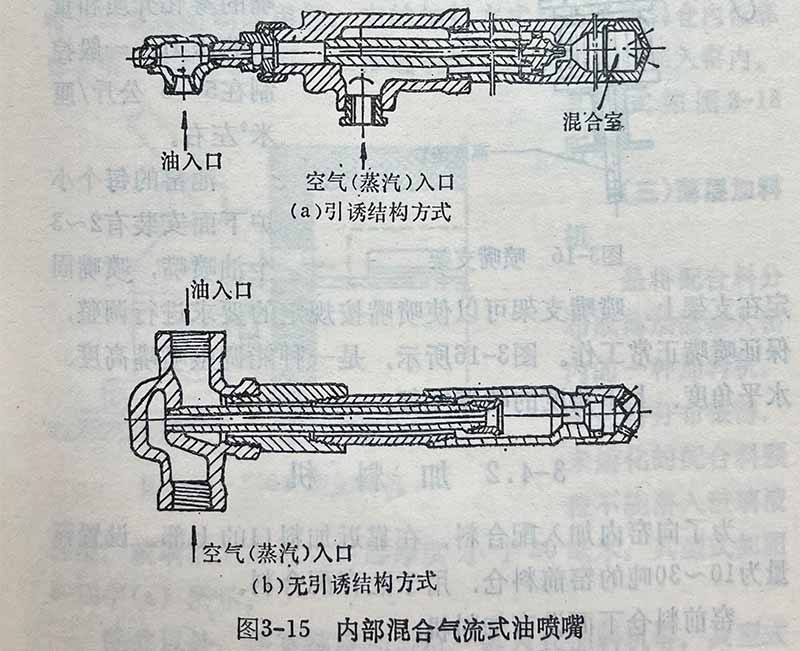
(2) Internal Mixing Stream Type Oil Burner Nozzle
This type atomizes the heavy oil after it is mixed with high-pressure air (compressed air) or superheated steam inside the nozzle (see Figure 3-15). A mixing chamber is provided at the nozzle head to mix the oil with compressed air or superheated steam. By replacing the nozzle tip at the outlet of the mixing chamber, the spray angle and the flame length of the oil burner nozzle can be changed. This type of nozzle is widely used and comes in many varieties. The heavy oil output of the internal mixing stream type nozzle is related to the working pressure of the atomizing medium, while the heavy oil output of the external mixing stream type nozzle is less affected by the working pressure of the atomizing medium. Therefore, the operation of the internal mixing stream type oil burner nozzle needs to be automatically controlled. The pressure of the atomizing medium and the heavy oil for the internal mixing stream type oil burner nozzle is generally controlled at about 5~6 kg/cm².
Each port of the furnace is equipped with 2~3 oil burner nozzles, which are fixed on a support. The nozzle support allows the nozzle to be adjusted according to the specified requirements to ensure normal operation. Figure 3-16 shows a nozzle support that can adjust the nozzle height, horizontal angle, and vertical angle.

1 – Batch Charger Opening 2 – Cullet 3 – Cullet Sprayer 4 – Cullet 5 – Slide 6 – Dense Batch Strip 7 – Roller 8 – Powdered Batch Material 9 – Hopper 10 – Screw Conveyor 11 – Exhaust Pipe
Batch Charger Machine
To introduce the batch materials into the furnace, a furnace-front silo with a capacity of 10~30 tons is set up above the batch charger opening to store the batch materials. A batch charger machine is installed below the furnace-front silo.
The batch charger machine has the following types:
(1) Electromagnetic Batch Charger
This type uses an electromagnetic vibrator to vibrate the batch charger, causing the batch materials falling from the silo to move sequentially towards the batch charger opening and be introduced into the furnace. Its type is shown in Figure 3-17.
(2) “162” Type Batch Charger
This type was first developed and used by Hartford in the United States. Its charging method is to continuously push the batch materials, which fall by gravity from the furnace-front silo, into the furnace through the batch charger opening using a pushing mechanism.
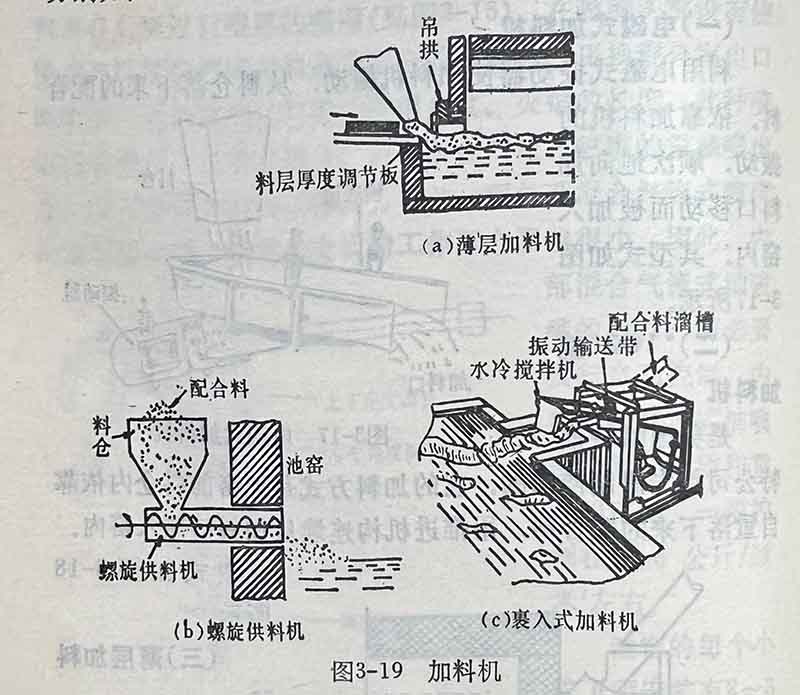
(3) Thin-Layer Batch Charger
This is a batch charger that disperses the batch materials into a thin layer and pushes them into the furnace. The batch materials are distributed very thinly, and unmelted batch particles cannot sink into the deep layer of the molten glass. The thickness of the batch layer on the molten glass surface is less than 30 mm. Its type is shown in Figure 3-19(a).
In addition, there are screw batch chargers and plunger-type batch chargers. Their types are shown in Figure 3-19(b) and (c), respectively.
The so-called dense batch charging method is a method of pressing the batch materials into a dense batch strip (about 20 mm thick) with a density of about 2.6 g/cm³ and directly feeding it into the furnace. The charging device is shown in Figure 3-20. Part of the gas in the batch materials is discharged from the exhaust pipe (11), and part is discharged when pressurized by the roller press (7). Cullet is covered on the cullet layer, and the dense batch strip is laid on the liquid surface. The dense batch strip can improve melting conditions, shorten melting time, reduce energy consumption, reduce batch segregation, and reduce the flying of powder. In addition, the screened fine powder can still be used. Therefore, the dense batch charging method has a promising future.
The most important aspect of batch charging is to constantly maintain a stable molten glass level and to keep the molten glass in the tank furnace in a good melting state. Therefore, while automatically measuring the molten glass level, the charging amount must be automatically regulated by interlocking with the opening and closing action of the batch charger machine.
Reversing Valve
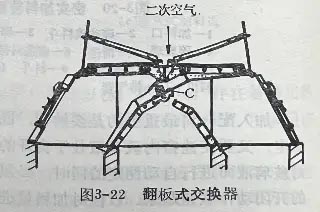
When a regenerator is used, waste gas flows into the regenerator chamber on one side, and secondary air flows into the regenerator chamber on the other side. At regular intervals, the flow of waste gas and secondary air in the two regenerator chambers must be reversed. The gas reversal is performed automatically. During the gas reversal, the oil burner nozzles are temporarily shut off. The device that changes the direction of the air and waste gas flow is called the Reversing Valve.
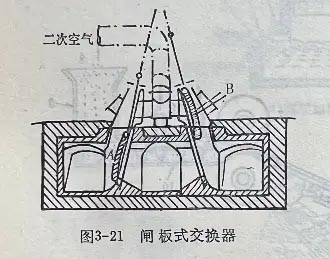
There are two types of reversing valves: slide-gate type and flap-gate type.
Figure 3-21 shows a slide-gate type reversing valve. It changes the direction of the air and waste gas flow by the alternating up and down movement of the A and B gates.
Figure 3-22 shows a flap-gate type reversing valve. It changes the direction of the air and secondary air waste gas by changing the direction of the valve plate around the C axis.
Chimney
After the reversing valve, a Chimney is installed at the end of the flue for exhausting the smoke. The reinforced concrete chimney is lined with refractory bricks inside.
Chimney Height: 40~60 meters
Chimney Inner Diameter: Upper part 1.3~2.5 meters, Lower part 2.1~3.4 meters
In addition, a waste heat boiler and pollution control equipment are usually installed between the reversing valve and the chimney via a bypass flue. The type and assembly of the equipment vary depending on the condition of the tank furnace.
Tank Furnace Cooling and Cooling Fan
The quality of the refractory materials used in the tank furnace has improved, reducing the degree of erosion of the refractory materials. However, during the long-term operation of the tank furnace, the refractory materials are still gradually thinned due to erosion. Especially the tank block part in contact with the molten glass surface is easily eroded and thinned because the temperature is too high.
From the perspective of melting, the temperature of the tank furnace should be kept very high. However, to extend the life of the refractory materials, cooling of the refractory materials is required. Especially for the tank block part in contact with the molten glass surface, forced cooling by blowing air must be strengthened to reduce the temperature and minimize the erosion of the tank block at that location by the molten glass. At the same time, special parts such as the throat and the corners of the batch charger opening also require special strengthening of cooling due to severe erosion.
The cooling air volume and power consumption for the relevant parts of the tank furnace are shown in Table 3-4:
Table 3-4 Cooling Air Volume and Power Consumption for Relevant Parts of the Tank Furnace
Cooling Location | Material / Type | Unit | Parameter | Japan | USA | USSR |
Tank wall | Clay brick | m | m³/min | 5–10 | 21–30 | 18–24 |
|
| kW/m | 0.25 | – | – |
|
Tank wall | Mullite electrofused cast brick | m | m³/min | 30–40 | 30–40 | 41.7–46.7 |
|
| kW/m | 0.7–0.9 | – | – |
|
Tank wall | Alumina–zirconia–silica (AZS) electrofused cast brick | m | m³/min | 40–60 | – | – |
|
| kW/m | 0.9–1.4 | – | – |
|
Throat | — | unit | m³/min | – | 112.5 | – |
Charging port corner | — | unit | m³/min | – | 50 | – |
The position of the cooling nozzle is generally 30~50 mm away from the furnace wall, recently reduced to 10~15 mm, and 40~50 mm below the liquid level. The exit velocity of the air nozzle is generally 30~40 m/s, and some even reach 70 m/s.
There are two main types of tank furnace forced air cooling systems: (1) Centralized air cooling system using a large blower; (2) Decentralized air cooling system using small blowers.
The specifications and number of tank furnace cooling fans depend on the required cooling air volume and the type of air cooling system. For example, a large glass tank furnace with a daily output of about 200 tons uses a centralized air cooling system with the following specifications for a large centrifugal fan:
Pressure: 250 mm water column
Air Volume: 800 m³/min
Power: 55 kW
The position of the cooling nozzle is generally 30~50 mm away from the furnace wall, recently reduced to 10~15 mm, and 40~50 mm below the liquid level. The exit velocity of the air nozzle is generally 30~40 m/s, and some even reach 70 m/s.
There are two main types of tank furnace forced air cooling systems: (1) Centralized air cooling system using a large blower; (2) Decentralized air cooling system using small blowers.
The specifications and number of tank furnace cooling fans depend on the required cooling air volume and the type of air cooling system. For example, a large glass tank furnace with a daily output of about 200 tons uses a centralized air cooling system with the following specifications for a large centrifugal fan:
Pressure: 250 mm water column
Air Volume: 800 m³/min
Power: 55 kW
Combustion Air Fan
The secondary air for combustion is naturally drawn into the regenerator chamber from the atmosphere through the air intake port at the bottom of the regenerator, driven by the suction of the waste gas discharged by the chimney or the exhaust fan.
If the amount of secondary air supplied by natural suction is insufficient or fluctuates too much, a separate Combustion Air Fan (or Blower) must be installed to force the secondary air into the regenerator chamber for preheating.
The combustion air fan is selected based on experience, and its air volume is generally 1.5 to 2 times the theoretically calculated air volume.
Measurement and Control of the Tank Furnace
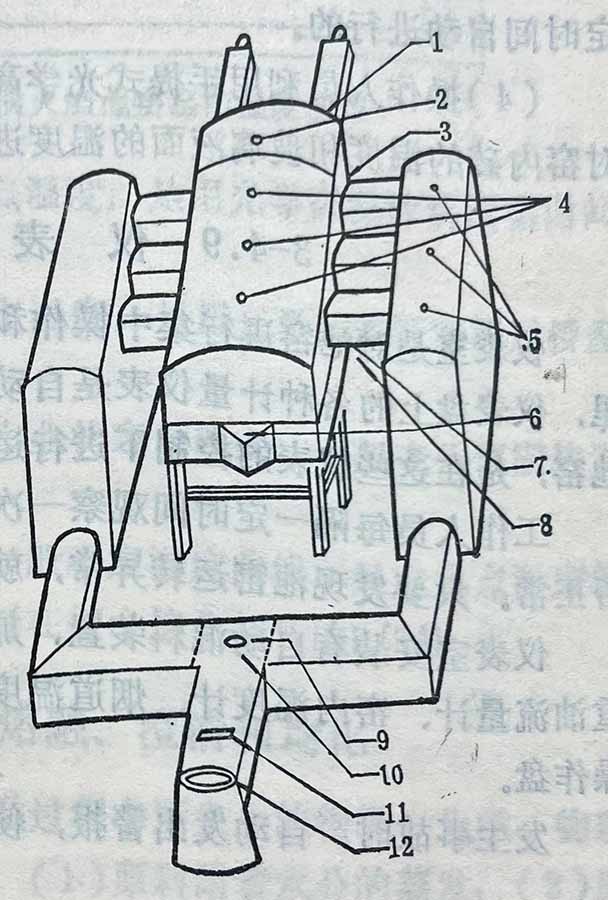
The measurement and control points and items of the tank furnace are shown in Figure 3-23.
1 – Liquid Level 2 – Working End Temperature 3 – Furnace Pressure 4 – Melting End Temperature 5 – Regenerator Crown Temperature 6 – Batch Charger 7 – Heavy Oil Pressure, Flow, Temperature 8 – Secondary Air Pressure 9 – Secondary Air 10 – Reversing Gate 11 – Furnace Pressure Regulating Damper 12 – Flue Temperature
(1) The liquid level measuring device is interlocked with the operation of the batch charger machine to automatically regulate the liquid level.
(2) The furnace pressure measuring device is interlocked with the operation of the furnace pressure regulating damper. If the furnace pressure fluctuates, the regulating damper on the main flue automatically operates to regulate the pressure.
(3) The reversal of the burner combustion and the gas reversal in the regenerator chamber are performed automatically at regular intervals.
(4) Operators use a portable optical pyrometer to measure the temperature of the furnace crown and the molten glass surface at regular intervals.
Instrument Room
The Instrument Room is the place for centralized operation and management of the tank furnace. Various measuring instruments on the instrument panel in the instrument room operate automatically. The automatic batch mixing equipment and the tank furnace operate under the control of these instruments. Operators observe the instruments at regular intervals to determine if the tank furnace is operating normally. If any abnormal operation of the tank furnace is found, measures should be taken to deal with it promptly.
The instrument room is equipped with control panels for automatic batch mixing equipment, batch charging equipment, molten glass level gauge, heavy oil flow meter, furnace temperature gauge, flue temperature gauge, automatic reversing device, and so on.
In case of an accident, an alarm is automatically issued so that the staff can deal with it in time.