


Operation and Repair of the Tank Furnace
Furnace Temperature Curve
The Furnace Temperature Curve is an important process control indicator for the tank furnace, which must not be arbitrarily changed and must be strictly kept stable.
The temperatures at points (1) and (2) in the figure are measured by an optical pyrometer observing the gap inside the furnace.
The temperatures at points (3) and (4) in the figure are measured by an optical pyrometer observing the bridge cover block.
These temperatures can be changed according to the operating conditions, and the general range of variation is about ±30℃.
For a horseshoe-flame tank furnace, a temperature curve is generally not set, only the temperature value and position of the hot spot are set. The hot spot position should be controlled at about 2/3 of the total length of the melting end.

Melting, Fining, and Homogenization
The physical, chemical, physicochemical phenomena, and reactions that occur during the melting of the glass batch materials are roughly: (1) Evaporation of the attached moisture in the raw materials; (2) Escape of gases such as CO2, SO2, and SO3 produced by the thermal decomposition of the raw materials; (3) Melting of low-melting components in the batch materials to form a liquid phase, and the formation of a multi-component liquid phase by eutectic components, with some local, special low-melting eutectic components also forming a liquid phase at low temperatures; (4) Mutual melting of the above various liquid phases, and the dissolution of unmelted solid components in the molten liquid; (5) Solid-state reactions between the raw materials, and between the generated silicate compounds and other oxides, to form new compounds; (6) Volatilization of certain components in the molten glass at high temperatures (such as K2O, Na2O, B2O3, PbO, SiF4, As2O3, etc.); (7) Dissolution of various gases covering the molten glass surface (combustion gases, air, and gases escaping from the thermal decomposition of raw materials) into the molten glass, and these dissolved gases turn back into small bubbles when saturation is reached. These phenomena and reactions do not necessarily occur in the above order, and some reactions occur simultaneously.
In the tank furnace, the batch materials on the molten glass surface flow longitudinally. Observing the position where the batch materials disappear on the molten glass surface can indicate the melting condition of the batch materials.
To prevent the production of unmelted batch materials and to obtain homogeneous molten glass, the melting of the batch materials must be completed as quickly as possible. The main factors affecting the melting time of the batch materials are: (1) Chemical composition of the glass; (2) Melting temperature and temperature distribution in the furnace; (3) Particle size and distribution of the raw materials; (4) Amount and particle size of cullet added; (5) Proportion of raw materials; (6) Uniformity of the batch materials; (7) Bubbling and electric boosting. The molten glass that has completed melting contains a large number of residual bubbles, and glass in this state cannot be used for forming. The process of removing these residual bubbles from the molten glass is called fining (or refining).
According to Stokes’ Law, the rising velocity of a bubble in molten glass can be expressed by the following formula:
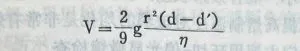
Where:
V — Rising velocity of the bubble (cm/s)
g — Acceleration due to gravity (cm/s^2)
r — Radius of the bubble (cm)
d — Density of the molten glass (g/cm^3)
d’ — Density of the gas in the bubble (g/cm^3)
η — Viscosity of the molten glass (g/cm·s)
When the temperature rises to the fining temperature, the viscosity of the glass decreases, the rising velocity of the bubbles increases, and the bubbles are more easily removed. However, the smaller the bubble, the more difficult it is to float up. Therefore, to accelerate fining, a fining agent should be added to the batch materials. In the tank furnace, the use of bubbling and electric boosting can also accelerate glass melting and fining. Small bubbles that cannot be removed during the fining process can be absorbed by the glass, become smaller, or disappear during the forming process as the temperature of the molten glass decreases and the gas pressure in the glass decreases.
The main factors affecting the fining quality of molten glass are: particle size of raw materials, batch material form, fining agent, refractory materials, impurities, temperature, and atmosphere. The specific method for controlling the fining quality of molten glass is to take samples at specific locations in the tank furnace, measure the number of bubbles in a certain amount of glass, and record and compare this with other conditions.
During the glass melting process, the molten glass is chemically non-uniform due to factors such as the volatilization of glass components and the erosion of refractory materials. The process of bringing the molten glass to a chemically uniform state is called homogenization of the molten glass.
The homogenization of molten glass is based on diffusion. The natural convection of the molten glass in the furnace plays a significant role in promoting the diffusion of the molten glass. This promoting effect can be enhanced by electric boosting, bubbling, or forced melting. Because the viscosity of molten glass is relatively high, melting, fining, and homogenization are not distinctly separate but occur simultaneously.
Flow of Molten Glass
The flow of molten glass in the tank furnace includes the forced outward flow caused by the drawing of glass, and the natural convection caused by the temperature difference. This convection of the molten glass serves to transfer heat from the surface of the molten glass to the low-temperature batch materials, tank blocks, and bottom. The convection of the molten glass is closely related to the temperature distribution and heat transfer in various parts of the tank furnace.
The flow of molten glass plays a significant role, both beneficial and detrimental, in the movement of the molten glass, unmelted batch materials, and bubbles in the tank furnace, as well as in the formation of glass, the homogenization of molten glass, and the erosion of refractory materials.
Therefore, understanding the position and distribution of the batch pile and the temperature gradient of the molten glass is very important for furnace operation.
Color Change of Molten Glass in the Tank Furnace
Due to sales requirements, it is sometimes necessary to change the color of the molten glass, which is unavoidable in a glass factory, but it is done only when necessary. When changing the color of the molten glass, a certain standard must be followed because problems can easily arise after the color change.
There are two methods for changing the color of molten glass in the tank furnace:
(1) Drain Method
The existing molten glass in the tank furnace is completely drained, and batch materials for the new color are added. The color change situations when using the drain method are shown in Table 3-5.
Table 3-5 Color Change Situations When Using the Drain Method
Previous Glass Color | New Glass Color |
Amber glass | Flint glass |
Dark green glass | Light green glass |
Flint glass | Amber glass |
Flint glass | Dark green glass |
Light green glass | Flint glass |
Dark green glass | Flint glass |
Light green glass | Dark green glass |
(2) Push-out Method
In this method, the existing molten glass in the tank furnace is not completely drained. Instead, the glass is drawn from the feeder channel while batch materials for the new color are continuously added to the furnace through the batch charger opening, gradually pushing out the existing molten glass. The color change situations when using the push-out method are shown in Table 3-6.
Table 3-6 Color Change Situations When Using the Push-out Method
Previous Glass Color | New Glass Color |
Amber Glass | Deep Green Glass |
Deep Green Glass | Light Green Glass |
Flint Glass | Amber Glass |
Flint Glass | Deep Green Glass |
Light Green Glass | Flint Glass |
Deep Green Glass | Light Green Glass |
Light Green Glass | Deep Green Glass |
The time required for changing the glass color in the tank furnace is 24~48 hours when using the push-out method, and 4 to 7 days when using the drain method. This time loss must be estimated in advance.
Campaign Life of the Tank Furnace
The period from the initial firing and heating of the tank furnace until the furnace is shut down and rebuilt is called the Campaign Life of the tank furnace.
The campaign life of the tank furnace is, in most cases, determined by the degree of wear of the tank block or the throat. If the tank block bricks or throat bricks are eroded by the molten glass over a long period, a hole may be created, and the molten glass will flow out of the hole, which is very dangerous. Therefore, the tank furnace must be shut down and rebuilt at this time.
During the operation of the tank furnace, the oil consumption increases year by year. The tank furnace may also need to be shut down and rebuilt due to increased oil consumption, decreased output, and decreased glass quality.
Recently, due to the use of zirconia crown bricks, the life of the tank furnace has reached 5~7 years. The life of the tank furnace varies depending on the type of glass being melted. The campaign life of a tank furnace melting amber glass is longer than that of a tank furnace melting flint glass.
Draining of the Tank Furnace
When the campaign life of the tank furnace is over and it is to be shut down, the molten glass in the tank furnace needs to be completely drained for easy dismantling of the furnace. This operation is called Draining.
If there is a wide area around the tank furnace, a pit can be dug, and a draining pool can be built with refractory bricks in the pit. A draining hole is opened in the lower part of the tank block in the melting end, and the molten glass flows out through a flow channel to the draining pool. The molten glass flows out through a draining hole lined with refractory bricks. It generally takes 5 hours to completely drain the molten glass in the tank furnace.
Recently, a small draining hole is opened in the tank block of the melting end or the bottom of the working end, and the molten glass is drained through a smaller flow channel at a speed of about 8~12 tons of glass per hour while being flushed with high-pressure water. Since it is difficult to open a draining hole in the tank block, the draining hole should be prepared during the construction of the furnace and blocked with bricks during the operation of the tank furnace. When changing the glass color, if the new glass color is completely different, the existing molten glass in the tank furnace should be completely drained. If very dirty molten glass accumulates at the bottom of the furnace or the feeder channel, a small draining hole needs to be chiseled open to drain it to improve the quality of the molten glass.
Repair and Rebuilding of the Tank Furnace
When the tank furnace is shut down for repair and rebuilding, all damaged bricks, except for the steel structure and foundation, need to be removed. If some bricks can still be used, they can be left and reused. It takes about 1 month to build a tank furnace with new bricks due to various factors. It takes about 25 days to build the regenerator chamber with bricks; it takes about 20 days to build the tank block, bottom, furnace wall, and main crown. The tank furnace is a key piece of equipment in a glass factory. The construction must be meticulous, strictly following the requirements of the relevant furnace construction specifications, and striving for perfection. Supplementary regulations can be made for the repair and rebuilding of certain special parts.
Heating-up of the Tank Furnace
After the tank furnace is built, it needs to be heated up before being put into production, gradually raising the temperature inside the furnace until the specified temperature is reached. This process is called Heating-up (or Frit-in).
For the heating-up of the tank furnace, easily combustible gaseous fuels such as city gas or liquefied petroleum gas are used first, followed by light oil. When the temperature inside the furnace rises to a temperature where heavy oil can easily burn, heavy oil is used for heating-up. When the brickwork inside the furnace is fully heated and reaches the specified temperature, cullet is added first, and then batch materials are gradually added for melting. When the specified amount is loaded, the heating-up time is over. With this heating-up method, the heating-up time for a 50-ton tank furnace is about 7 days, and for a 300-ton tank furnace, it is about 14 days. To fill the tank furnace with molten glass to the specified liquid level (25~50 mm below the top of the tank block), it takes 1~2 days for a 50-ton tank furnace and 4~5 days for a 300-ton tank furnace. The heating-up curve of the tank furnace is shown in Figure 3-25.
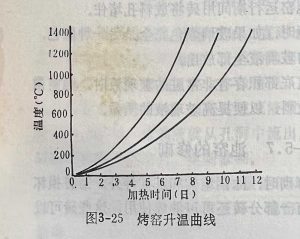
The three tank furnace heating-up curves shown in the figure require 8 days, 10 days, and 12 days, respectively, for the temperature inside the furnace to rise from room temperature to 1450℃. In recent years, the fast heating-up method has been promoted abroad.
The fast heating-up method uses positive pressure high-temperature hot gas flow to enhance the heat transfer effect of the furnace brickwork. Jet-type burners that can stabilize the flame are used to spray a large amount of hot gas flow into the furnace. Even if the pressure inside the furnace is very high, the heating-up can be carried out normally, and the temperature can be rapidly increased from 100 to 1400 ℃ in any furnace type. This method has two outstanding advantages: (1) Fast heating-up shortens the heating-up time and allows for earlier production; (2) The temperature rises uniformly during the heating-up process, reducing the damage to refractory materials caused by rapid cooling and heating. When using the fast heating-up method, the heating-up time for a tank furnace with a melting area of 36~96 ㎡ is 72 hours, and for a tank furnace with a melting area larger than this, it is 96 hours. According to statistics, as of March 1970, 311 tank furnaces in the United States had adopted the fast heating-up method, of which 195 were glass bottle and jar tank furnaces.